I Bought the Part. The Part Was Right. So Why Did It Still Cost Us $2,100?
I'm the office administrator at an 85-person manufacturing company. I manage all MRO ordering—roughly $180,000 annually across 14 vendors. I report to both operations and finance.
About a third of what I order is electrical control equipment: Yaskawa VFDs, contactors, relays, timers, PLC modules. Not glamorous procurement. Just the stuff that keeps the floor running.
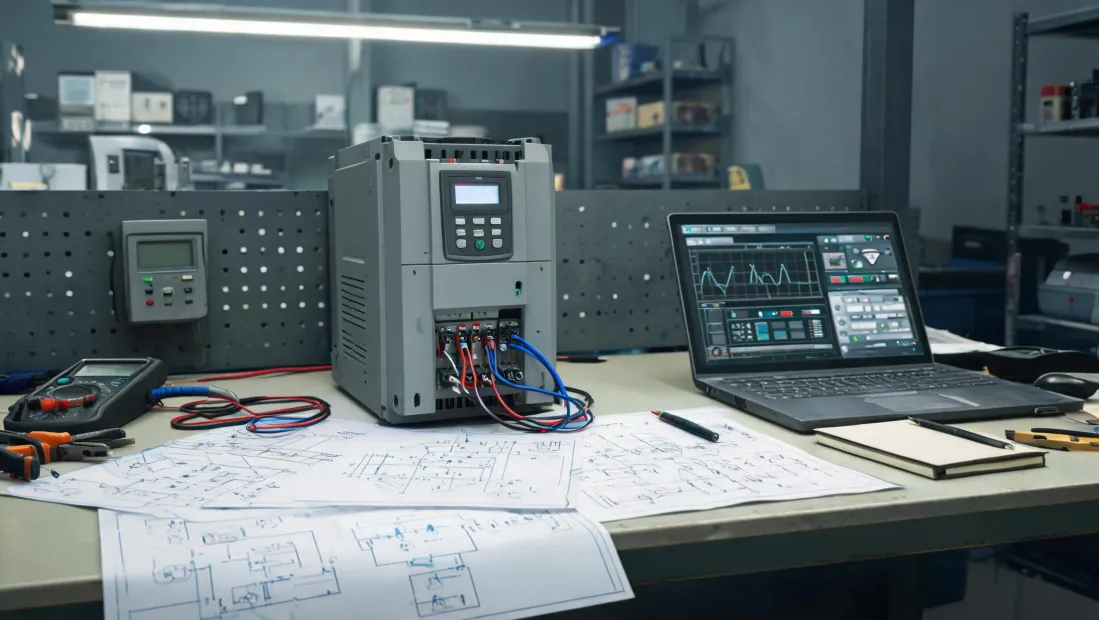
Three months ago, I placed a $340 order for a Yaskawa VFD to replace a burnt-out unit. It arrived on time. It sat on the maintenance shelf for nine days. Why? The paperwork that shipped with it didn't include the matching data we needed to align it with our existing contactor specifications. We ordered the companion parts again. Waited eleven more days.
That $340 order turned into a $2,100 bill and roughly nine hours of downtime.
I've been through this cycle enough times now that I stopped blaming the vendor.
Everyone Thinks This Is a Pricing Problem. It Isn't.
When I talk to other admins and procurement people in our industry, the complaints are always the same. "Vendors are gouging us." "This brand costs 20% more than that one." "We need to negotiate harder."
I get it. Price is easy. You can benchmark it. You can negotiate it annually. Your CFO can understand it in a spreadsheet.
But price is the only part of procurement that's visible. The part that actually kills you happens after the order is placed: the gap between what the spec sheet says and what actually fits together on your floor.
That's what happened with my VFD order. And it's the reason most maintenance managers are quietly frustrated three months after every spare parts shipment.
How the Gap Actually Forms
Here's what nobody in this industry says out loud: most procurement people are not engineers. But the people placing orders for technical parts are expected to read technical documents with engineering-level judgment.
That's it. That's the whole problem, hiding in plain sight at every small company I've ever worked with.
Let me break down how this plays out.
Spec sheets are written per-product, not per-system
Yaskawa VFDs have solid documentation. Contactor specifications are usually well-laid-out—amp ratings, coil voltage, auxiliary contacts, mounting. PLC specification guides will tell you I/O count, scan time, communication protocol.
What they rarely tell you is how these things behave together in your specific panel.
A VFD's "recommended companion contactor" might have a coil voltage that doesn't match the contactor you already have installed. A timer datasheet—pick any timer manufacturer—won't tell you that its reset time conflicts with the model you're replacing. The PLC spec guide will be technically accurate and still leave you guessing about whether the existing wiring harness matches.
So you buy what looks like a matched set. What you actually bought were parts that are individually correct and collectively incompatible.
"Compatible" is a marketing word, not an engineering word
This is where I get a bit frustrated.
Here's something vendors won't tell you: "compatible" usually means "it fits," not "it works in your application."
Per FTC advertising guidelines (ftc.gov), claims need to be truthful and substantiated. Most vendors are pretty careful about this. But "compatible with Yaskawa VFDs" is a claim made in a vacuum—in the context of a single SKU, not your panel, your wiring, or your existing control chain.
You need system-level compatibility. Vendors sell component-level compatibility. That mismatch is where most orders go wrong.
Wait—the real problem wasn't the vendor at all
I didn't fully understand any of this until the vendor failure in March 2023 forced me to look at our own records.
I pulled 18 months of return and rework log. Two-thirds of our "wrong part" incidents traced back to one thing: we never wrote the system requirement down. We only wrote down part numbers.
We bought the Yaskawa VFD because it was a good VFD. We bought the contactor because its specs looked right. We never once verified on-site that the two would talk to each other.
It took me three years and about 140 purchase orders to understand that you're not buying parts. You're buying an outcome. And the spec sheet is the thinnest possible line between you and that outcome.
What the Gap Actually Costs You
This is the part I've started tracking more carefully, because I report to operations and finance. When specs fail, the cost isn't linear. It compounds in three layers.
Layer 1: The rework cost
Expedited shipping on the reorder. Restocking fees on the return. The administrative time to redo the PO. In my experience, that runs $150 to $400 per incident at our scale. Not catastrophic. But it happens over and over.
Layer 2: The downtime cost
This is where it stings. Depending on where in the production line a control failure happens, a shift hour of downtime can cost anywhere from $400 to $2,400—a wide range, I know, but factor in overtime to catch up and the customer calls, and it climbs.
My $340 order with the missing spec sheet cost us roughly $2,100 to $2,400 all-in, if I count internal labor honestly. If that failure had hit a higher-throughput station, the number would have been twice that.
Layer 3: The accounting friction layer
This is the one that embarrasses you in front of the finance director. Missing documentation. Invoices that don't reconcile. Cost allocation that nobody can defend. Rejected expense reports.
I once ate $2,400 out of a department budget because of this exact pattern. Now I verify invoicing capability before placing any order. Every time.
The Fix, Briefly
I'll keep this short, because the diagnosis is the hard part.
One: ask about the system, not the part. Instead of "is this Yaskawa VFD compatible with our existing drive?", ask "what's the matched drive/contactor/timer combination for our application?" Yaskawa VFD tech support exists for a reason. Use it before you buy, not after.
Two: treat spec guides as a starting point, not an answer. Any PLC specification guide or contactor specification sheet should be cross-referenced against what's actually on your floor. Someone with eyes on the panel needs to sign off.
Three: small orders deserve the same honesty as big ones. When I was starting out, the vendors who treated my $200 orders seriously are the ones I still use for $20,000 orders. The minimum order quantity was never the issue. The issue was whether anyone would spend twenty minutes verifying that my $340 part would actually fit into my system.
I can only speak to our size of operation—around 140 mid-range orders a year, mostly VFDs, contactors, timers, and PLC modules. If you're running a much larger integration shop with dedicated engineers, this probably sounds obvious. But if you're in a 50-100 person company, sitting between operations and finance, trying to figure out why your spares budget keeps leaking—this is probably where it's going.
Worth checking. The spec gap doesn't announce itself. It just shows up on the invoice.